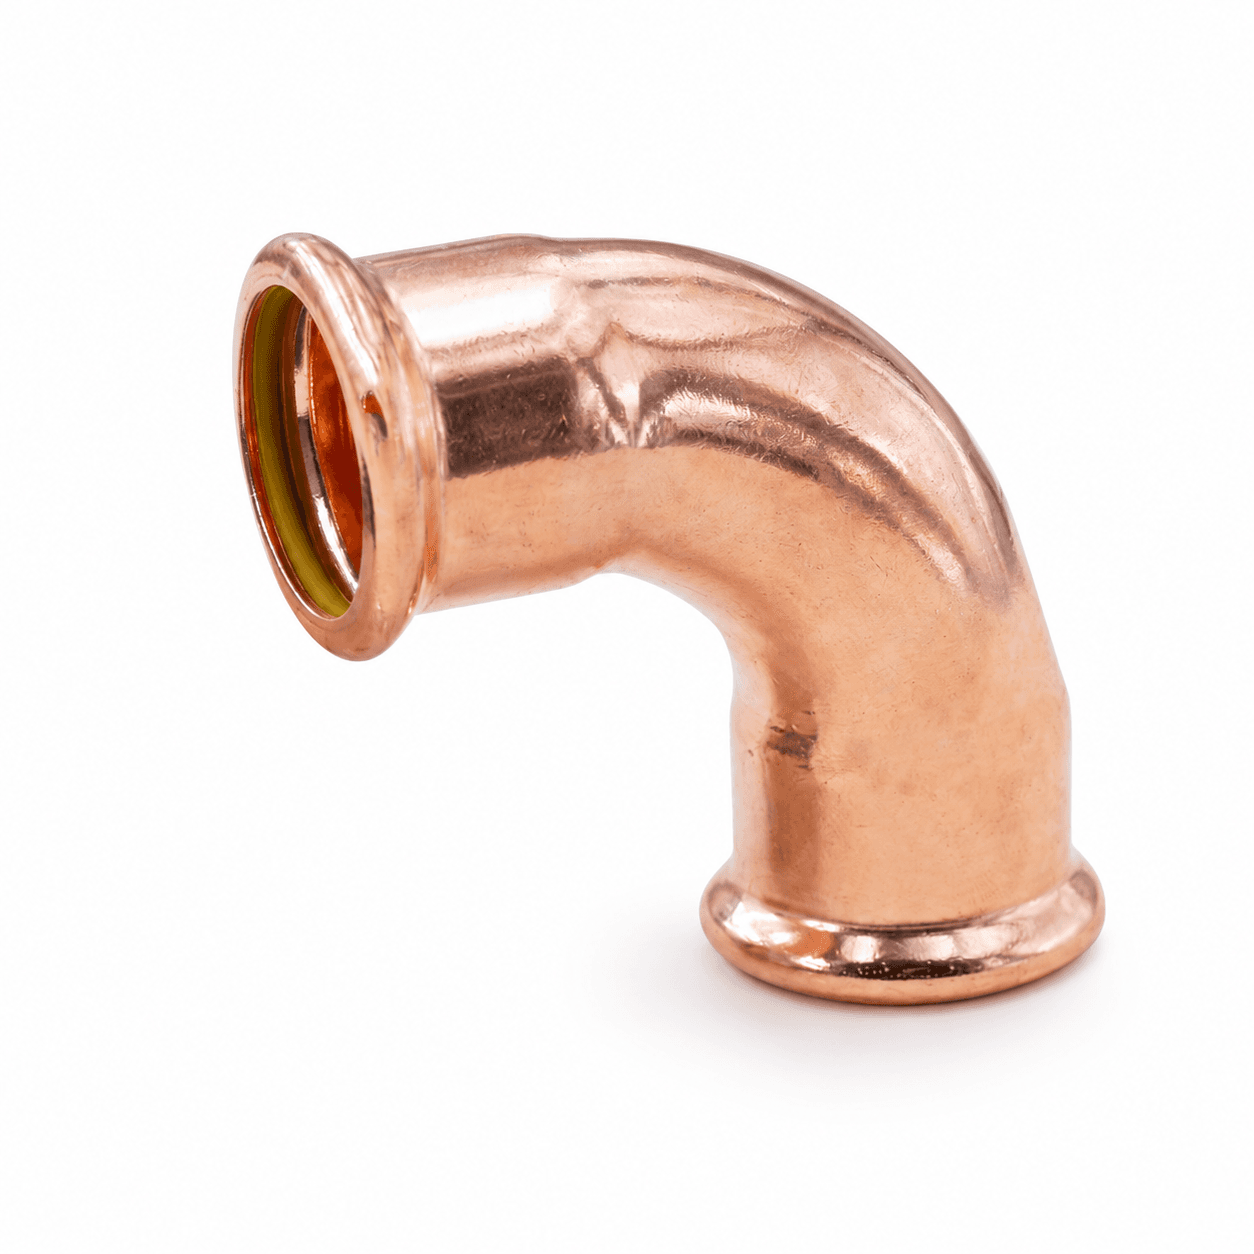
Pressfit Gas 90 Degree Elbow
Pressfit Gas 90 Degree Elbow
Product Options
| SKU | SIZE / OPTION | AVAILABILITY | PRICE | QTY | ACTION |
|---|---|---|---|---|---|
| PG - 13 | IN STOCK | £1.02 Ex. VAT | |||
| PG - 13 - P10 | IN STOCK | £10.20 Ex. VAT | |||
| PG - 13 - P20 | IN STOCK | £19.60 Ex. VAT | |||
| PG - 13 - P30 | IN STOCK | £28.61 Ex. VAT | |||
| PG - 14 | IN STOCK | £2.44 Ex. VAT | |||
| PG - 14 - P10 | IN STOCK | £24.40 Ex. VAT | |||
| PG - 14 - P20 | IN STOCK | £46.90 Ex. VAT | |||
| PG - 14 - P30 | IN STOCK | £68.45 Ex. VAT | |||
| PG - 15 | IN STOCK | £1.82 Ex. VAT | |||
| PG - 15 - P10 | IN STOCK | £18.20 Ex. VAT | |||
| PG - 15 - P20 | IN STOCK | £34.98 Ex. VAT | |||
| PG - 15 - P30 | IN STOCK | £51.06 Ex. VAT | |||
| PG - 16 | IN STOCK | £3.13 Ex. VAT | |||
| PG - 16 - P10 | IN STOCK | £31.30 Ex. VAT | |||
| PG - 16 - P20 | IN STOCK | £60.16 Ex. VAT | |||
| PG - 16 - P30 | IN STOCK | £87.81 Ex. VAT | |||
| PG - 17 | IN STOCK | £3.44 Ex. VAT | |||
| PG - 17 - P10 | IN STOCK | £34.40 Ex. VAT | |||
| PG - 17 - P20 | IN STOCK | £66.12 Ex. VAT | |||
| PG - 17 - P30 | IN STOCK | £96.50 Ex. VAT | |||
| PG - 18 | IN STOCK | £4.65 Ex. VAT | |||
| PG - 18 - P10 | IN STOCK | £46.50 Ex. VAT | |||
| PG - 18 - P20 | IN STOCK | £91.55 Ex. VAT | |||
| PG - 18 - P30 | IN STOCK | £135.95 Ex. VAT | |||
| PG - 19 | IN STOCK | £4.41 Ex. VAT | |||
| PG - 19 - P10 | IN STOCK | £44.10 Ex. VAT | |||
| PG - 19 - P20 | IN STOCK | £84.76 Ex. VAT | |||
| PG - 19 - P30 | IN STOCK | £123.71 Ex. VAT | |||
| PG - 20 | IN STOCK | £7.21 Ex. VAT | |||
| PG - 20 - P10 | IN STOCK | £72.10 Ex. VAT | |||
| PG - 20 - P20 | IN STOCK | £138.58 Ex. VAT | |||
| PG - 20 - P30 | IN STOCK | £202.26 Ex. VAT | |||
| PG - 21 | IN STOCK | £10.79 Ex. VAT | |||
| PG - 21 - P10 | IN STOCK | £107.90 Ex. VAT | |||
| PG - 21 - P20 | IN STOCK | £207.38 Ex. VAT | |||
| PG - 21 - P30 | IN STOCK | £302.69 Ex. VAT |
Quick Trade Summary: Copper M-Profile Press Fit Gas 90° Elbow
MEP Stock supplies heavy-duty copper press fit 90° gas elbows engineered for natural gas, LPG, and compressed air installations. Fabricated from premium CW024A / DHP deoxidised copper, each fitting is fitted with factory-lubricated yellow HNBR (Hydrogenated Nitrile Butadiene Rubber) O-rings designed to resist aromatic hydrocarbons. Full M-profile mechanical press geometry guarantees a permanent, gas-tight joint in seconds without naked flames, soldering, or hot works permits.
High-Performance Copper Press Gas 90-Degree Elbows for Gas Safe Engineers
Designed for domestic, commercial, and industrial gas pipework, our M-Profile 90° press fit gas elbows provide a 100% mechanical, flame-free directional change for copper pipework conforming to BS EN 1057 (R250 half-hard / R290 hard). Under the Gas Safety (Installation and Use) Regulations 1998 (GSIUR) and BS 6891 specifications, installing fuel gas lines in confined voids, timber-framed constructions, and occupied commercial facilities often makes open brazing or soldering hazardous. MEP Stock gas press fittings eradicate hot work permits, fire watch delays, and system flux contamination.
Engineering Specifications & Material Standards
| Parameter | Specification Standard |
|---|---|
| Fitting Body Material | Deoxidised High Phosphorus Copper CW024A / Cu-DHP (BS EN 1254-7) |
| Elastomeric Sealing Element | High-Grade Yellow HNBR (Hydrogenated Nitrile Butadiene Rubber) |
| Press Profile Compatibility | M-Profile Press Jaws (Rothenberger, Novopress, Milwaukee, Rems, Klauke) |
| Operating Pressure (Gas) | Max 5 bar (MOP 5 / PN5) for Natural Gas & LPG vapor systems |
| Operating Temperature Range | -20°C to +70°C (-4°F to 158°F) |
| Safety Feature | Leak-Before-Press (LBP) design reveals unpressed fittings during pressure testing |
| Applicable UK Statutory Standards | BS 6891, BS EN 1254-7, IGEM/UP/2, Gas Safety (GSIUR 1998) |
Step-by-Step Gas Press Installation Guide
- Square Tube Cut: Cut BS EN 1057 copper pipe cleanly at 90° using a rotary pipe cutter. Never use a hacksaw.
- Internal & External Deburring: Thoroughly deburr both the inner and outer tube edges using a calibrated deburring reamer. A sharp tube burr will lacerate the yellow HNBR O-ring during insertion, invalidating the seal.
- Insertion Depth Marking: Measure and clearly mark the insertion depth onto the copper tube using a permanent marker or depth gauge.
- Visual Seal Inspection: Ensure the yellow HNBR seal is cleanly seated in the fitting toroidal groove and free of metal filings or grit.
- Mechanical Pressing: Slide the fitting over the pipe until it hits the internal stop. Mount calibrated M-profile jaws perpendicular to the fitting bead and cycle the press tool completely until the mechanical crimp is executed.
- Tightness Testing: Conduct statutory gas tightness testing in accordance with BS 6891 / IGEM/UP/1B before commissioning.
Frequently Asked Questions: Copper Gas Press 90° Elbows
Can I use a water press fitting on a gas pipework installation?
No, absolutely not. Water press fittings use black EPDM O-rings, which degrade rapidly when exposed to fuel gas hydrocarbons. Under BS 6891 and the Gas Safety (Installation and Use) Regulations 1998 (GSIUR), gas installations strictly require dedicated press-fit gas fittings fitted with factory-installed yellow HNBR (Hydrogenated Nitrile Butadiene Rubber) seals and clearly marked with external yellow identification.
Can press-fit gas fittings be buried in concrete screed or solid floors under BS 6891?
Under BS 6891, mechanical press joints must not be directly embedded in concrete screed or solid floors without an accessible duct or protective sleeve. Gas pipework embedded in screed should be continuous unjointed soft-coiled copper (factory pre-insulated) or installed within an accessible ducted channel. Where press joints are located under floors or in ceiling voids, they must remain readily accessible for inspection and leak detection.
What is the minimum safe distance between a press fitting and an existing soldered joint?
Maintain a minimum distance of at least 100mm (or 3x pipe diameter for larger sizes) from existing soldered capillary joints, and always complete hot works first. If soldering near an installed press fitting, open flames or conducted heat exceeding 70°C will thermally degrade and destroy the internal yellow HNBR rubber O-ring. Always allow the soldered joint to cool completely to room temperature before inserting and pressing the adjacent fitting.
What press jaw profile do I need for MEP Stock copper gas fittings?
These fittings strictly require M-Profile press jaws. Standard UK press tools equipped with M-contour jaws—such as Rothenberger (Compact / Twin Turbo), Milwaukee (M12 / M18 Force Logic), Novopress (ACO103 / ACO203), and REMS (Mini-Press / Power-Press)—will execute the certified hexagonal crimp. Do not use V-profile or U-profile jaws on M-profile fittings.
What is the minimum pipe clearance required between two consecutive press fittings?
For 15mm and 22mm copper pipe, leave a minimum clearance gap of 10mm to 15mm between the fitting collars; for 28mm to 54mm, leave at least 20mm. This clearance ensures the press tool jaws seat squarely over the fitting bead without colliding with the adjacent fitting's shoulder or causing pipe ovality during the mechanical crimp cycle.
How does the Leak-Before-Press (LBP) feature work during gas tightness testing?
The yellow HNBR O-ring features an engineered bypass channel that deliberately leaks air or test gas at low testing pressures (10 to 50 mbar) if unpressed. During the mandatory pre-commissioning tightness test (under BS 6891 / IGEM/UP/1B), an unpressed joint reveals an immediate pressure drop on your digital manometer or U-gauge, preventing unpressed joints from going unnoticed before fuel gas is introduced.
Stock Up on Trade Gas Press Fittings Today
Available in 15mm, 22mm, 28mm, 35mm, 42mm, and 54mm in singles or discounted bulk trade packs of 10, 20, and 30. Order online at MEP Stock.
Quick Trade Summary: Copper M-Profile Press Fit Gas 90° Elbow
MEP Stock supplies heavy-duty copper press fit 90° gas elbows engineered for natural gas, LPG, and compressed air installations. Fabricated from premium CW024A / DHP deoxidised copper, each fitting is fitted with factory-lubricated yellow HNBR (Hydrogenated Nitrile Butadiene Rubber) O-rings designed to resist aromatic hydrocarbons. Full M-profile mechanical press geometry guarantees a permanent, gas-tight joint in seconds without naked flames, soldering, or hot works permits.
High-Performance Copper Press Gas 90-Degree Elbows for Gas Safe Engineers
Designed for domestic, commercial, and industrial gas pipework, our M-Profile 90° press fit gas elbows provide a 100% mechanical, flame-free directional change for copper pipework conforming to BS EN 1057 (R250 half-hard / R290 hard). Under the Gas Safety (Installation and Use) Regulations 1998 (GSIUR) and BS 6891 specifications, installing fuel gas lines in confined voids, timber-framed constructions, and occupied commercial facilities often makes open brazing or soldering hazardous. MEP Stock gas press fittings eradicate hot work permits, fire watch delays, and system flux contamination.
Engineering Specifications & Material Standards
| Parameter | Specification Standard |
|---|---|
| Fitting Body Material | Deoxidised High Phosphorus Copper CW024A / Cu-DHP (BS EN 1254-7) |
| Elastomeric Sealing Element | High-Grade Yellow HNBR (Hydrogenated Nitrile Butadiene Rubber) |
| Press Profile Compatibility | M-Profile Press Jaws (Rothenberger, Novopress, Milwaukee, Rems, Klauke) |
| Operating Pressure (Gas) | Max 5 bar (MOP 5 / PN5) for Natural Gas & LPG vapor systems |
| Operating Temperature Range | -20°C to +70°C (-4°F to 158°F) |
| Safety Feature | Leak-Before-Press (LBP) design reveals unpressed fittings during pressure testing |
| Applicable UK Statutory Standards | BS 6891, BS EN 1254-7, IGEM/UP/2, Gas Safety (GSIUR 1998) |
Step-by-Step Gas Press Installation Guide
- Square Tube Cut: Cut BS EN 1057 copper pipe cleanly at 90° using a rotary pipe cutter. Never use a hacksaw.
- Internal & External Deburring: Thoroughly deburr both the inner and outer tube edges using a calibrated deburring reamer. A sharp tube burr will lacerate the yellow HNBR O-ring during insertion, invalidating the seal.
- Insertion Depth Marking: Measure and clearly mark the insertion depth onto the copper tube using a permanent marker or depth gauge.
- Visual Seal Inspection: Ensure the yellow HNBR seal is cleanly seated in the fitting toroidal groove and free of metal filings or grit.
- Mechanical Pressing: Slide the fitting over the pipe until it hits the internal stop. Mount calibrated M-profile jaws perpendicular to the fitting bead and cycle the press tool completely until the mechanical crimp is executed.
- Tightness Testing: Conduct statutory gas tightness testing in accordance with BS 6891 / IGEM/UP/1B before commissioning.
Frequently Asked Questions: Copper Gas Press 90° Elbows
Can I use a water press fitting on a gas pipework installation?
No, absolutely not. Water press fittings use black EPDM O-rings, which degrade rapidly when exposed to fuel gas hydrocarbons. Under BS 6891 and the Gas Safety (Installation and Use) Regulations 1998 (GSIUR), gas installations strictly require dedicated press-fit gas fittings fitted with factory-installed yellow HNBR (Hydrogenated Nitrile Butadiene Rubber) seals and clearly marked with external yellow identification.
Can press-fit gas fittings be buried in concrete screed or solid floors under BS 6891?
Under BS 6891, mechanical press joints must not be directly embedded in concrete screed or solid floors without an accessible duct or protective sleeve. Gas pipework embedded in screed should be continuous unjointed soft-coiled copper (factory pre-insulated) or installed within an accessible ducted channel. Where press joints are located under floors or in ceiling voids, they must remain readily accessible for inspection and leak detection.
What is the minimum safe distance between a press fitting and an existing soldered joint?
Maintain a minimum distance of at least 100mm (or 3x pipe diameter for larger sizes) from existing soldered capillary joints, and always complete hot works first. If soldering near an installed press fitting, open flames or conducted heat exceeding 70°C will thermally degrade and destroy the internal yellow HNBR rubber O-ring. Always allow the soldered joint to cool completely to room temperature before inserting and pressing the adjacent fitting.
What press jaw profile do I need for MEP Stock copper gas fittings?
These fittings strictly require M-Profile press jaws. Standard UK press tools equipped with M-contour jaws—such as Rothenberger (Compact / Twin Turbo), Milwaukee (M12 / M18 Force Logic), Novopress (ACO103 / ACO203), and REMS (Mini-Press / Power-Press)—will execute the certified hexagonal crimp. Do not use V-profile or U-profile jaws on M-profile fittings.
What is the minimum pipe clearance required between two consecutive press fittings?
For 15mm and 22mm copper pipe, leave a minimum clearance gap of 10mm to 15mm between the fitting collars; for 28mm to 54mm, leave at least 20mm. This clearance ensures the press tool jaws seat squarely over the fitting bead without colliding with the adjacent fitting's shoulder or causing pipe ovality during the mechanical crimp cycle.
How does the Leak-Before-Press (LBP) feature work during gas tightness testing?
The yellow HNBR O-ring features an engineered bypass channel that deliberately leaks air or test gas at low testing pressures (10 to 50 mbar) if unpressed. During the mandatory pre-commissioning tightness test (under BS 6891 / IGEM/UP/1B), an unpressed joint reveals an immediate pressure drop on your digital manometer or U-gauge, preventing unpressed joints from going unnoticed before fuel gas is introduced.
Stock Up on Trade Gas Press Fittings Today
Available in 15mm, 22mm, 28mm, 35mm, 42mm, and 54mm in singles or discounted bulk trade packs of 10, 20, and 30. Order online at MEP Stock.
You May Also Like
 Featured
Brass Compression Straight Coupling
 Featured
Solder Ring Reducing Coupling Copper Plumbing Pipe Fitting
 Featured
Copper Endfeed Equal Tee WRAS Approved Pipe Fitting
 Featured
Copper Endfeed Stop End Cap WRAS Approved Copper Pipe Fitting
 Featured
Chrome Compression Reducing Tee WRAS Approved Plumbing Pipe Fitting
Rubber Lined Pipe Clips with Blue Safety Lock
Copper Two-Piece Pipe Spacing Clips